BLOG
Knowledge
Technology and Services
What are the technical requirements for penstock pipes in pumped-storage hydropower?
2026-07-22
What is a Penstock?
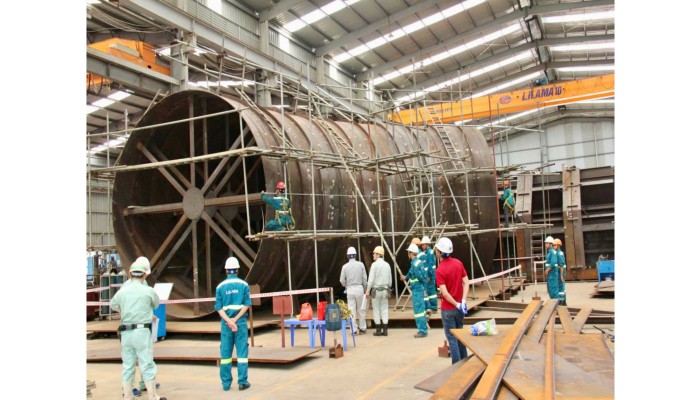
A penstock is a closed conduit or pipeline used to convey water from a reservoir, surge tank, or intake to the turbine of a hydropower plant. In a pumped-storage hydropower system, water is circulated between two reservoirs at different elevations:
- When electricity demand is low, surplus electricity is used to pump water from the lower reservoir to the upper reservoir.
- When electricity demand increases, water from the upper reservoir is directed down through the turbine to generate electricity.
Because the same water conduit can be involved in both power generation and water pumping, pressure-bearing components must operate under frequently changing flow, pressure, and operating conditions. Pumped-storage hydropower is therefore likened to a large-scale electricity storage system.
How does a penstock in pumped-storage hydropower differ from a conventional pipeline?
Compared to conventional industrial pipelines, penstocks in pumped-storage hydropower must withstand high water pressure, transient pressure due to water hammer, and repetitive loads as the system switches between pumping and power generation modes. Additionally, large diameters and thick steel plates make requirements for roundness, edge misalignment, weld quality, and deformation control more stringent. Therefore, penstocks need to be designed and fabricated as critical pressure-bearing steel structures, rather than merely being considered conventional water pipelines.
Key technical requirements for penstock pipelines
Comprehensive determination of design loads
Before selecting materials or thickness, the design entity must comprehensively determine all possible load combinations acting on the pipeline. Loads typically considered include:
| Load Group | Content to be Evaluated |
| Operating Pressure | Pressure during power generation, pumping, and transition modes |
| Transient Pressure | Water hammer during valve opening/closing or flow changes |
| Self-weight | Pipe body, coating, accessories, and water in the pipe |
| Thermal Load | Expansion, contraction, and temperature differences |
| Seismic Load | Depending on project location and requirements |
| Foundation Displacement | Settlement, movement at supports or anchor blocks |
| External Pressure | Soil, rock, groundwater, or vacuum inside the pipe |
| Construction Load | Lifting, transportation, fit-up, and hydrostatic testing |
| Fatigue Load | Pumping, generation, start-up, and shutdown cycles |
One important point is that the design pressure should not simply be taken as the normal operating pressure. The final value must be determined based on transient hydraulic analysis, adverse operating conditions, and safety factors according to applicable standards.
Selection of suitable materials
Materials for penstock fabrication typically must simultaneously meet the following requirements:
- Appropriate yield strength and tensile strength.
- Impact toughness at design temperature.
- Good weldability.
- Controlled chemical composition.
- Uniformity between steel batches.
- Crack resistance during welding.
- Formability when rolling thick steel plates.
- Complete material certification documentation.
For high-strength steel, increasing the yield strength can help reduce thickness and structural weight. However, the higher the material strength, the more stringent the requirements for welding technology, heat input, preheating temperature, and hydrogen control. Therefore, material selection should not be based solely on nominal strength. Simultaneous evaluation is needed for:
- Availability.
- Fabricability.
- Fabricator's welding capability.
- Inspection requirements.
- On-site repair conditions.
- Lifecycle cost.
Welding process control
Welding is one of the critical steps determining penstock quality. The pipeline may include:
- Longitudinal welds of each pipe section.
- Circumferential welds between sections.
- Welds at conical sections.
- Welds of curved sections.
- Branch welds.
- Welds connecting to flanges, stiffener rings, or anchor details.
Before manufacturing, the fabricator must develop and approve welding procedures suitable for:
- Steel grade.
- Thickness.
- Joint type.
- Welding position.
- Welding method.
- Type of welding material.
- Ambient temperature conditions.
- Post-weld mechanical property requirements.
Parameters that need to be controlled during welding include:
- Preheating temperature.
- Interpass temperature.
- Heat input.
- Welding speed.
- Welding sequence.
- Holding time.
- Storage conditions for welding electrodes and flux.
- Cleaning between passes.
- Post-weld distortion.
For thick steel plates or high-strength steel, controlling diffusible hydrogen is particularly important in reducing the risk of cold cracking.
Deformation control during rolling and welding
In penstock fabrication, deformation can occur at various stages:
- Blank cutting.
- Steel plate rolling.
- Fit-up of longitudinal welds.
- Multi-pass welding.
- Pipe section assembly.
- Stiffener ring welding.
- Welding of conical or branch sections.
- Lifting and transportation.
Without early control measures, post-weld reshaping can increase costs, affect schedules, and potentially degrade material quality. Commonly considered solutions include:
- Calculation of deformation compensation.
- Design of appropriate jigs and fixtures.
- Rational division of welding sections.
- Symmetric or balanced welding.
- Control of welding sequence.
- Limiting heat input.
- Geometric measurement at each stage.
- Use of suitable rotating, fixturing, and lifting equipment.
- Only perform thermal straightening according to approved procedures.
For large-diameter components, inspection should not only be performed after completion. Intermediate inspection points should be arranged to detect deviations before they accumulate.
Non-destructive testing of welds
Penstock welds must be inspected according to the scope, methods, and acceptance criteria specified in the design documentation or project standards. Commonly used methods include:
- Visual Testing – VT.
- Penetrant Testing – PT.
- Magnetic Particle Testing – MT.
- Ultrasonic Testing – UT.
- Radiographic Testing – RT.
- Phased Array Ultrasonic Testing – PAUT.
- Time-of-Flight Diffraction – TOFD.
Each method has its own scope of application and limitations. Selection should be based on:
- Joint type.
- Thickness.
- Material.
- Component geometry.
- Type of defect to be detected.
- Two-sided accessibility.
- Data storage and retrieval requirements.
TOFD and PAUT offer advantages in recording inspection data and evaluating defects by depth. However, they do not automatically replace all other methods. The NDT plan must be developed as a system tailored to the specific requirements of the project. The U.S. Bureau of Reclamation also maintains specific guidelines for inspecting steel penstocks and pressure conduits, indicating that lifetime inspection activities are a critical part of structural safety management.
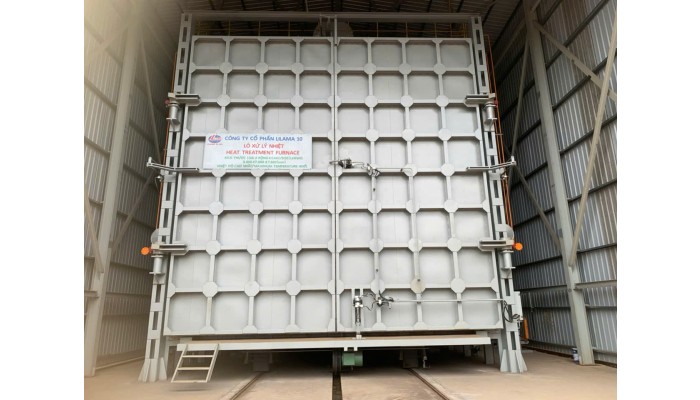
Consideration of post-weld heat treatment requirements
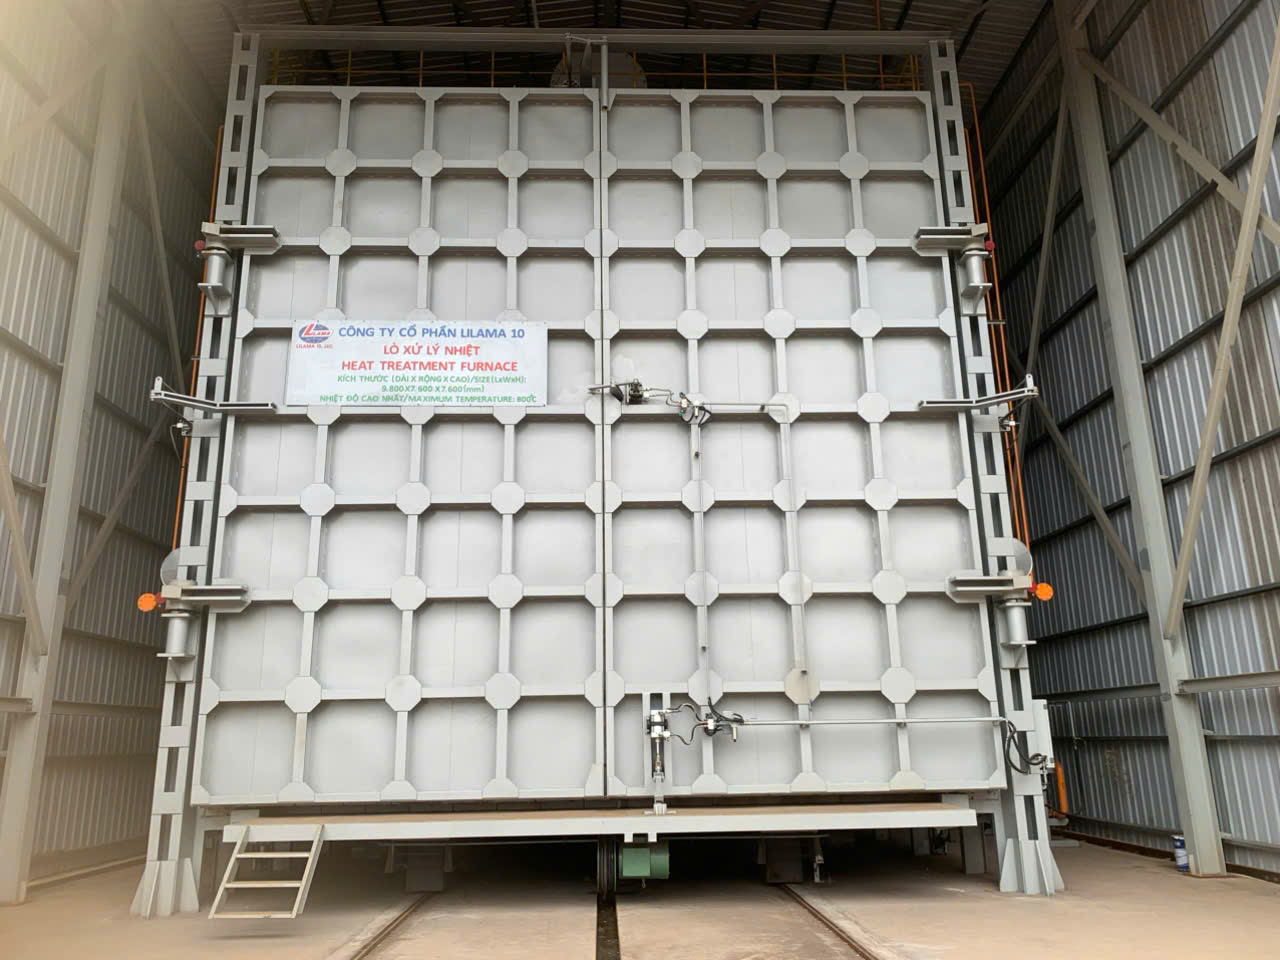
PWHT – Post Weld Heat Treatment is a post-welding heat treatment process aimed at controlling residual stresses or improving the condition of the weld zone in appropriate cases. However, it should not be assumed that all penstock welds require PWHT. This requirement depends on:
- Material.
- Thickness.
- Joint type.
- Design standard.
- Mechanical property requirements.
- Stress state.
- Operating conditions.
- Specific owner's regulations.
For large-sized components, if PWHT is required, the difficulty is not only in achieving the temperature. The fabricator must also control:
- Heating rate.
- Temperature difference between locations.
- Soaking time.
- Cooling rate.
- Placement of thermocouples.
- Recording and storing temperature charts.
- Deformation during treatment.
- Capability for full or local treatment.
Corrosion protection
Penstocks can be affected by:
- Water and humidity.
- Dissolved oxygen.
- Sediment and solid particles.
- Surrounding soil or rock environment.
- Groundwater.
- Condensation on the outer surface.
- Limited ventilation conditions.
- Corrosion at damaged coating locations.
The surface protection system needs to be selected based on:
- Whether the penstock is exposed or buried.
- Water conditions.
- Flow velocity.
- Accessibility for maintenance.
- Design life.
- Fabrication and on-site construction conditions.
For the inner surface of the pipeline, the coating must be simultaneously considered for its adhesion, water immersion resistance, flow resistance, and repair conditions.
Quality control and document traceability
For penstocks, quality inspection is not just about final product acceptance. Each pipe section needs to be traceable from raw material input to the final inspection results. The quality documentation package may include:
- Material certificates.
- Cutting diagrams and heat number traceability.
- Welding procedure specifications (WPS).
- Welder and NDT personnel certifications.
- Dimensional inspection reports.
- Welding log.
- Temperature charts.
- NDT reports.
- Weld repair records.
- Cleaning and painting records.
- Acceptance reports.
- As-built drawings.
Digitizing records and attaching identification codes to each pipe section helps reduce the risk of errors during:
- Transportation.
- On-site staging.
- Sequential installation.
- Joint verification.
- Maintenance after the facility becomes operational.
Design for transportation and installation
A penstock section may fully meet fabrication requirements but still pose significant challenges if not designed appropriately for logistics and site conditions. From the initial fabrication sectioning stage, consideration should be given to:
- Lifting capacity of cranes and site equipment.
- Permissible dimensions for road or waterway transportation.
- Lifting lug positions.
- Rigidity during transportation.
- Potential for deformation during support.
- Installation sequence.
- Location of field welds.
- NDT access space.
- Ventilation and safety conditions inside the pipeline.
- Feasibility of coating repair after welding.
For conical sections, curved sections, branch connections, or complex-shaped components, the factory fit-up plan should simulate actual conditions as closely as possible.
Lifetime inspection and maintenance
After commissioning, penstocks still require periodic inspection. Areas that typically need attention include:
- Welds.
- Supports.
- Anchor blocks.
- Curved sections.
- Transition sections.
- Branch connections.
- Areas in contact with foundation or concrete.
- Areas with leakage or condensation.
- Areas with coating degradation.
Inspection activities may include:
- Visual observation.
- Thickness measurement.
- Coating inspection.
- Weld inspection at suspicious locations.
- Deformation monitoring.
- Leak detection.
- Assessment of abnormal vibrations.
- Comparison with operational data.
Due to the repetitive loading characteristics of pumped-storage hydropower, cycle count data and operational history are also valuable in assessing the pipeline's condition.
LILAMA 10's capabilities in fabricating pressure pipelines and steel structures for pumped-storage hydropower
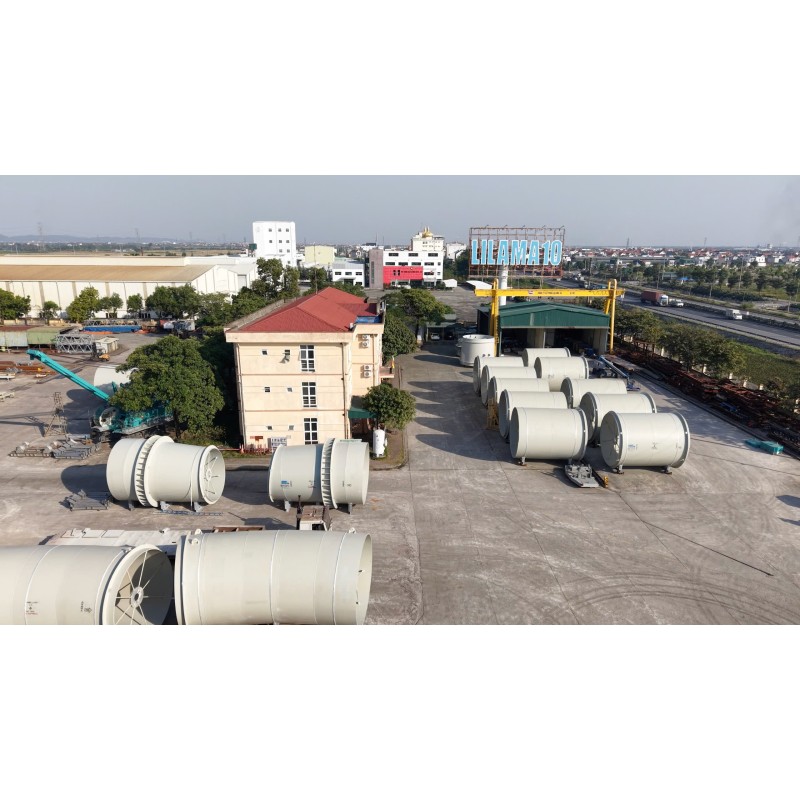
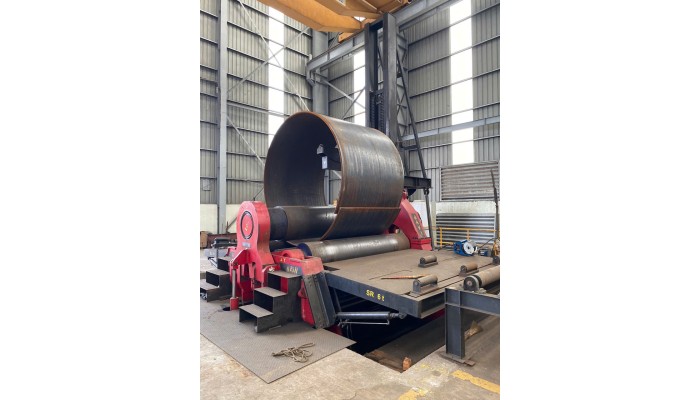
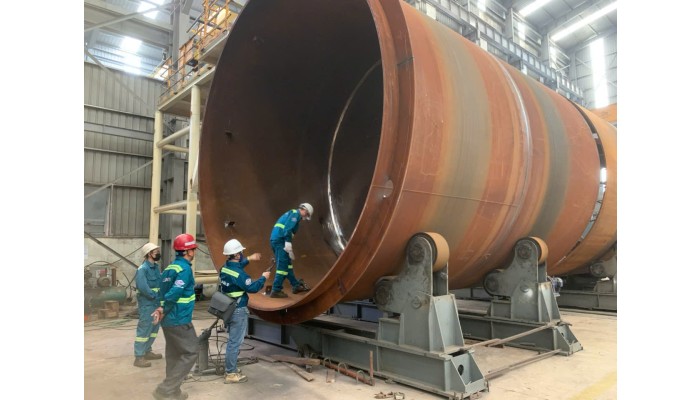
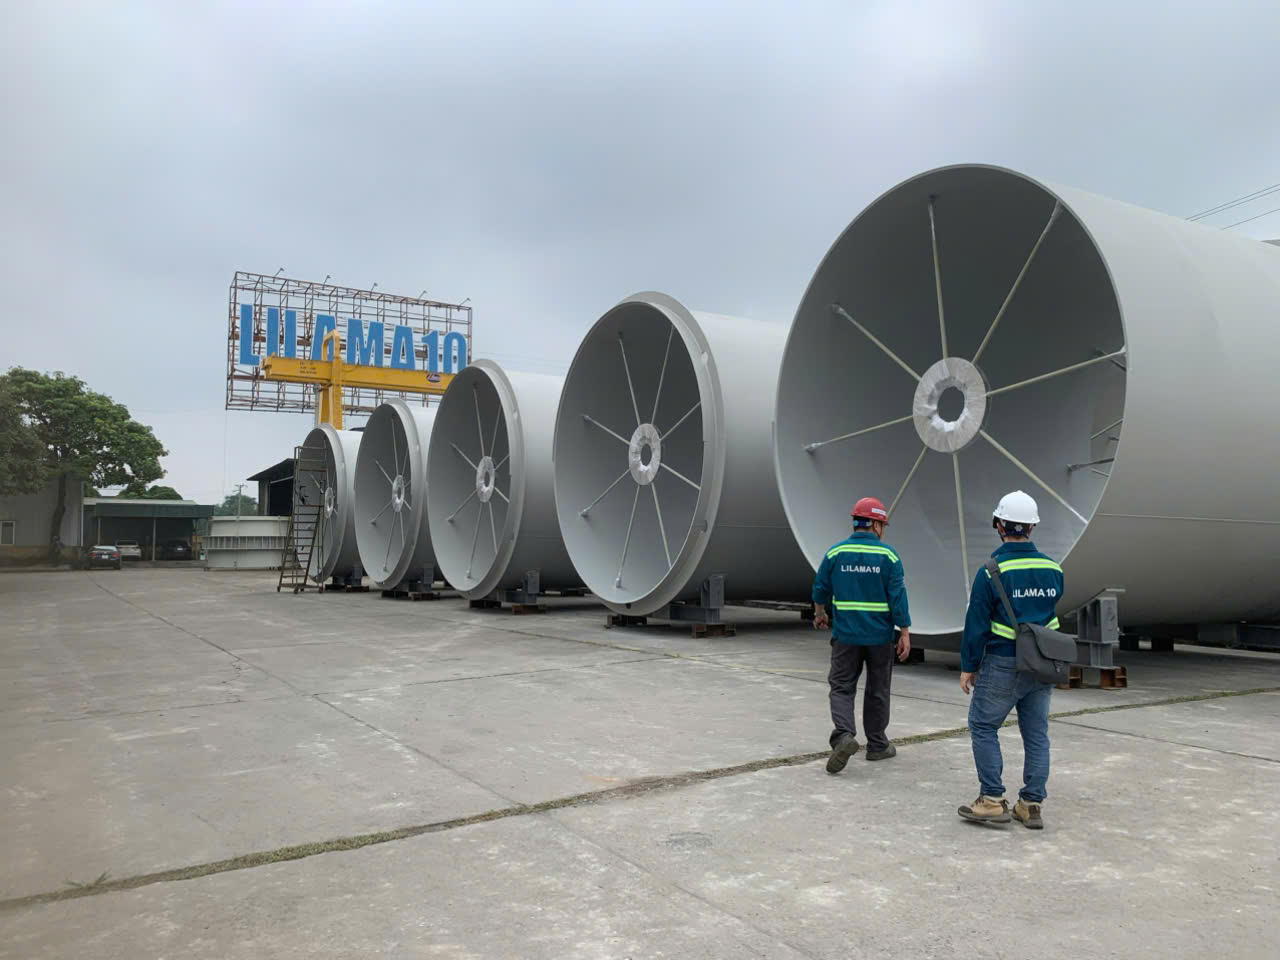
With experience participating in numerous hydropower and energy projects, LILAMA 10 has accumulated capabilities in fabricating and installing large-scale pressure pipelines and steel structures, meeting stringent quality and schedule requirements. The company has participated in projects such as Nam Ngum (Laos), Nam Theun 1, Ialy Expansion, Tri An Expansion, and is currently executing the Bac Ai Pumped-Storage Hydropower Project. In addition to its workshop system and equipment for large-scale steel structure fabrication, LILAMA 10 also synchronously implements non-destructive testing (NDT, TOFD), post-weld heat treatment (PWHT) technologies, and quality control procedures throughout the manufacturing process. These are crucial capabilities that enable the company to meet the requirements for penstocks and pressure equipment in modern hydropower projects.
Company Information
Construction Installation / Office Rental
LILAMA10 Joint Stock Company is a leading enterprise in manufacturing, installation, and technical services for civil, industrial, transportation, and infrastructure projects.To meet the demands and c ...
PICKUP
Technology & Services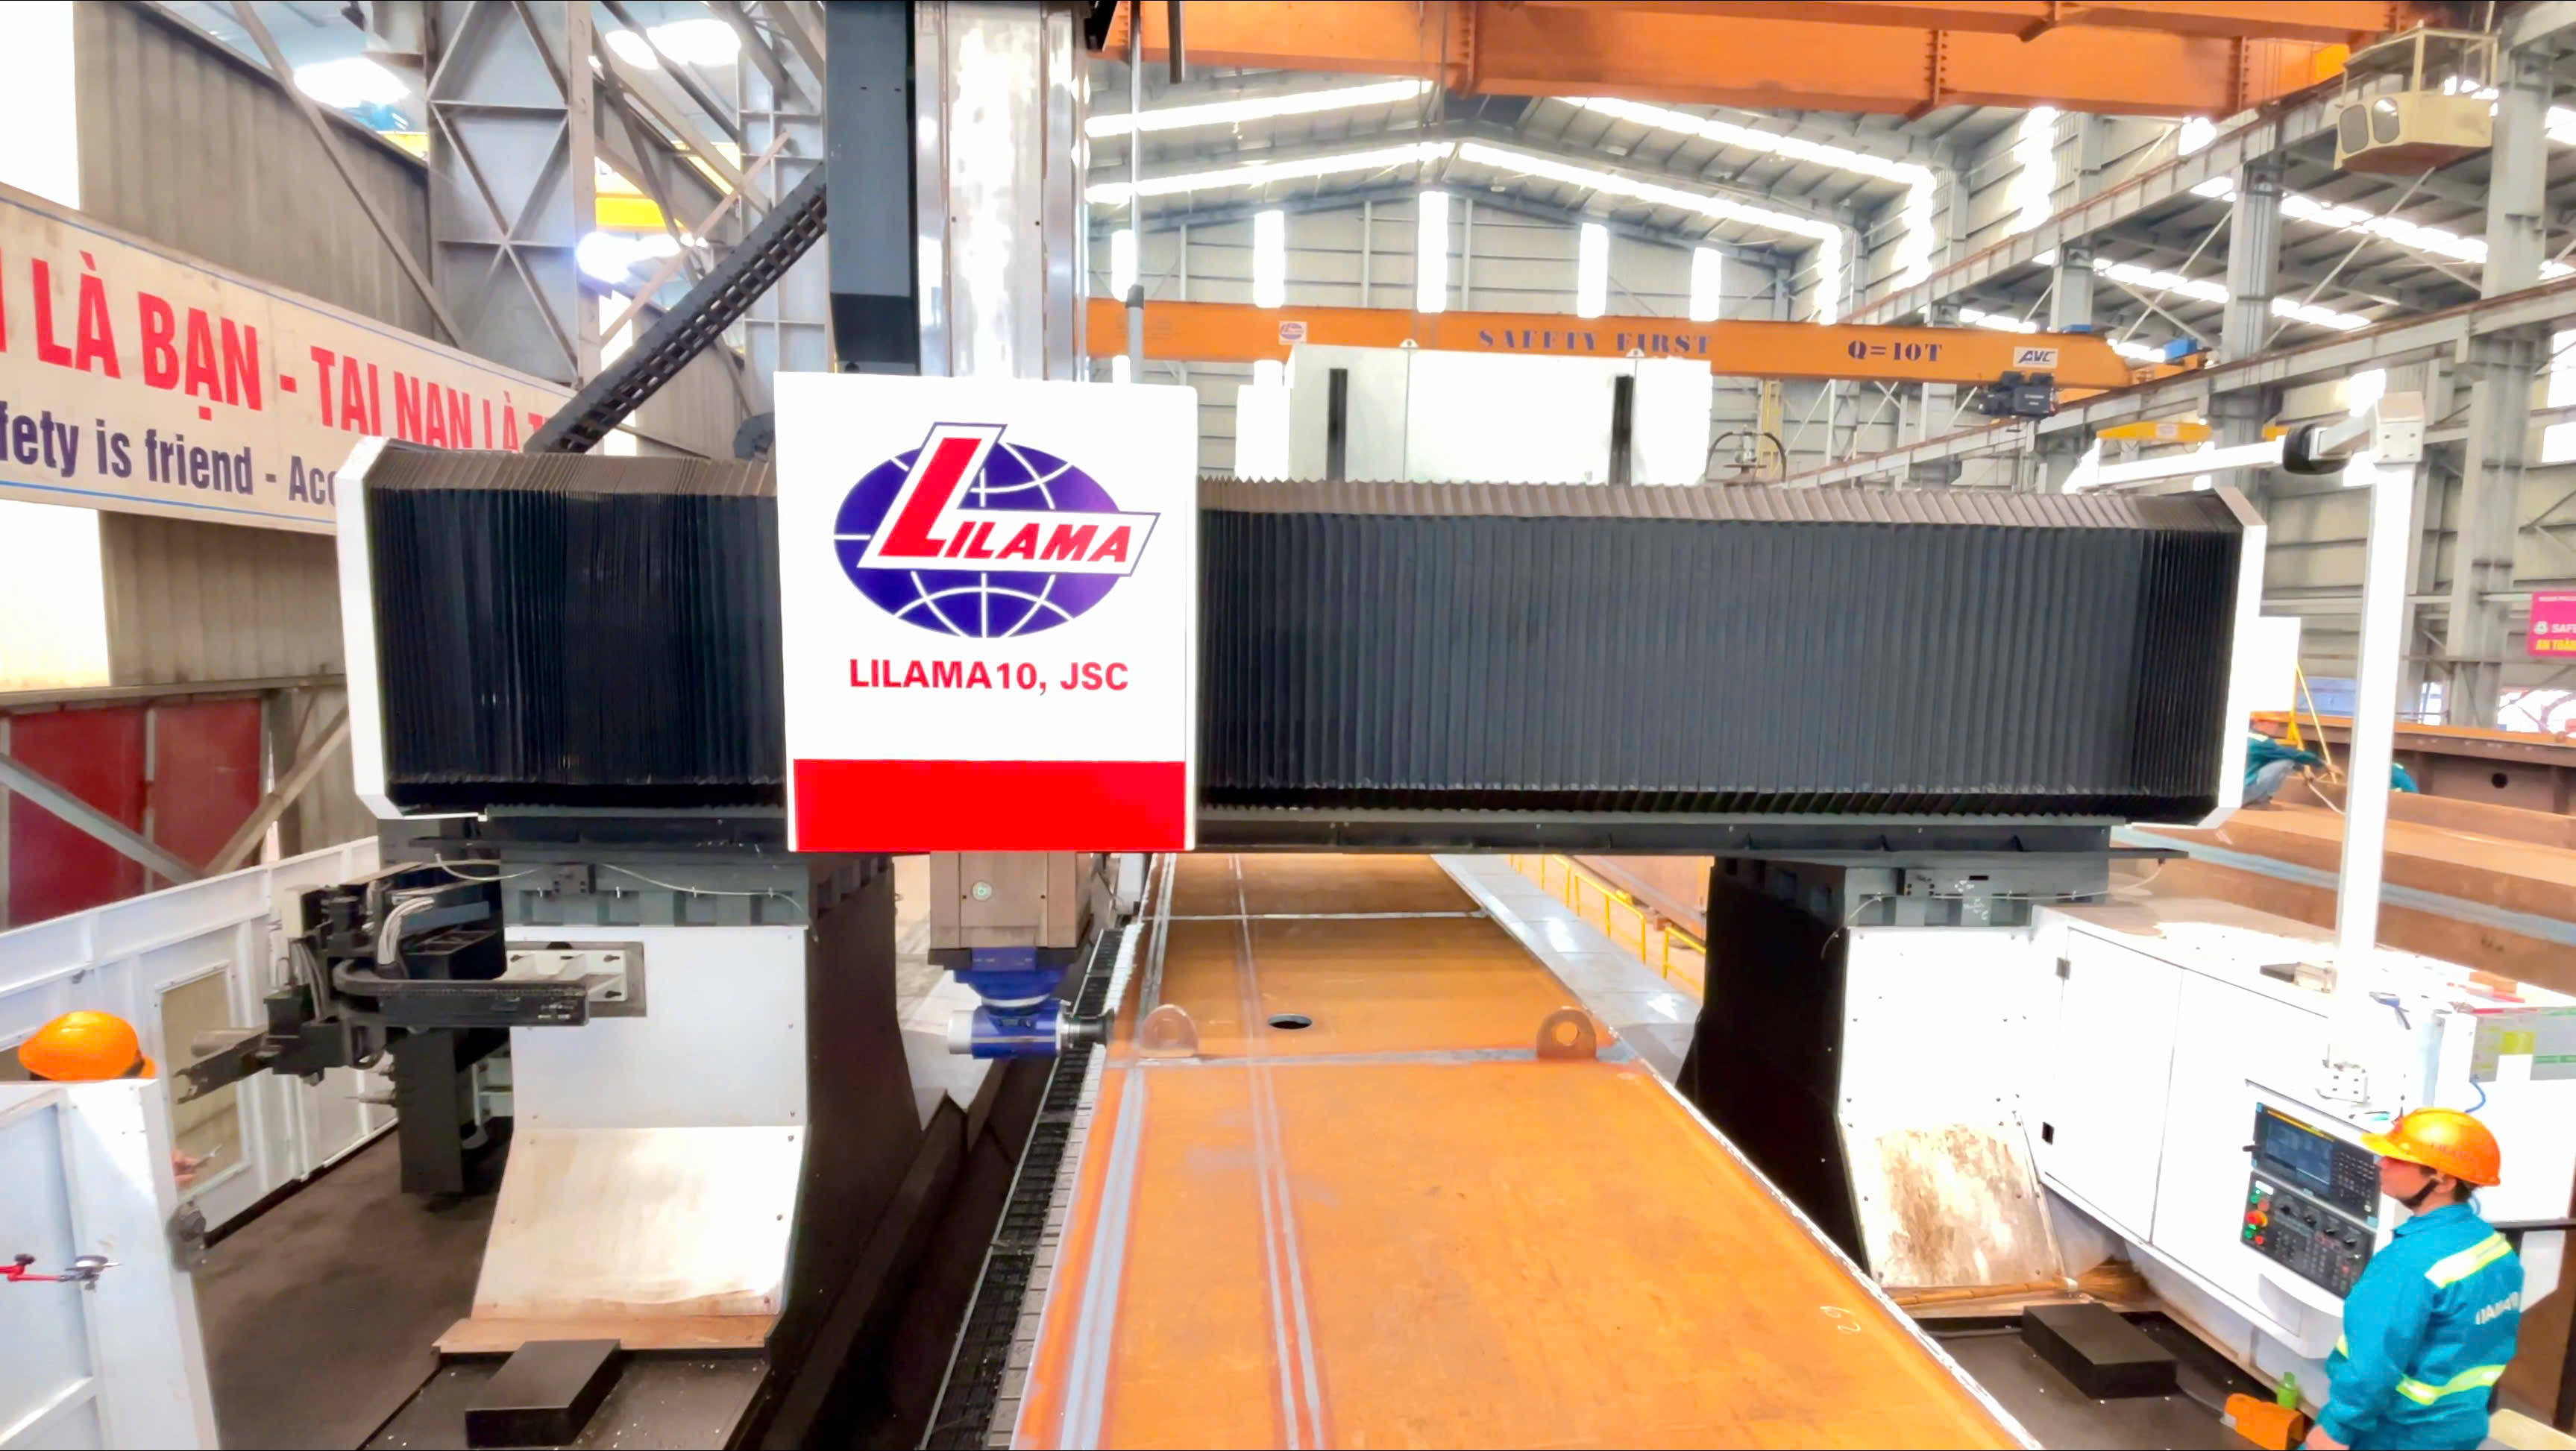
CONTACT
Contact