BLOG
Knowledge
Technology and Services
Warpage defects in sand casting: Causes and solutions to reduce casting deformation
2026-05-13
Warping Defects in Sand Casting
Causes and Solutions to Limit Casting Deformation
In sand casting, especially for large-sized or thin-walled FC and FCD cast iron products, warping is a common defect that directly affects geometric accuracy, assembly capability, and the quality of post-machined products.If not well controlled, warping can cause dimensional deviations in castings, generate residual stress, and significantly increase the cost of post-casting correction or machining.So, what causes castings to warp? How can deformation be limited during the sand casting process?
What is Warping Defect in Sand Casting?
Warping defect is the phenomenon where a casting changes its shape or dimensions compared to the original design after solidification and cooling.This defect often occurs when:
- The product structure lacks sufficient rigidity
- Shrinkage rates between different areas are uneven
- Internal stresses develop within the casting during crystallization and cooling
In many cases, castings can be bent, twisted, or locally deformed even if the initial dimensions meet requirements.
What is Internal Stress in Castings?
During solidification, liquid metal transforms into a solid state and begins to shrink.However:
- Thick and thin sections cool unevenly
- Some areas shrink first, others later
- Temperature differences create tensile forces within the casting
These forces are called residual stress or internal stress in castings.If the stress exceeds the part's deformation resistance, the casting will warp after removal from the mold or during machining.
Causes of Warping Defects in Sand Casting
1. Unreasonable Casting Structure
Parts with thin walls, large lengths, or open structures often have poor deformation resistance. When thermal shrinkage occurs during cooling, the casting is prone to bending or local twisting.
2. Warped Pattern
If the pattern or core box does not ensure accuracy, shape deviations will be directly transferred to the casting.
3. Suboptimal Gating System Design
Improper metal flow and heat distribution can cause localized shrinkage and generate residual stress.An unreasonable gating system causes heat to concentrate in certain areas, leading to significant differences in cooling times between regions.This is a common cause of warping in plate-like, long, or asymmetrical parts.
4. Inappropriate Cooling and Demolding
Premature demolding or uneven cooling causes the casting to deform before its dimensions have stabilized.
Phenomena and Effects of Casting Warping Defects
Warping defects can cause numerous problems in mechanical manufacturing and assembly:
- Castings are bent, twisted, or misshapen
- Dimensional and flatness deviations
- Failure to meet assembly tolerances
- Increased machining allowance for correction
- Additional straightening or heat treatment steps
- Increased scrap rate in mass production
For products requiring high precision or those exported to Japan and the US, warping defects can cause products to fail quality standards.
Solutions to Limit Warping Defects in Sand Casting
To minimize casting warping, foundries often implement multiple technical solutions simultaneously:
- Design balanced casting structures and increase rigidity
- Calculate an appropriate gating system to control heat distribution
- Casting simulation before mold manufacturing
- Control uniform cooling rates between different areas
- Avoid premature demolding when the casting is not yet stable
- Regularly check the accuracy of patterns and core boxes
Good control from design to gating technology and cooling significantly reduces deformation and stabilizes product quality.
DISOCO's Sand Casting Solutions Help Limit Warping Defects and Stabilize Casting Dimensions
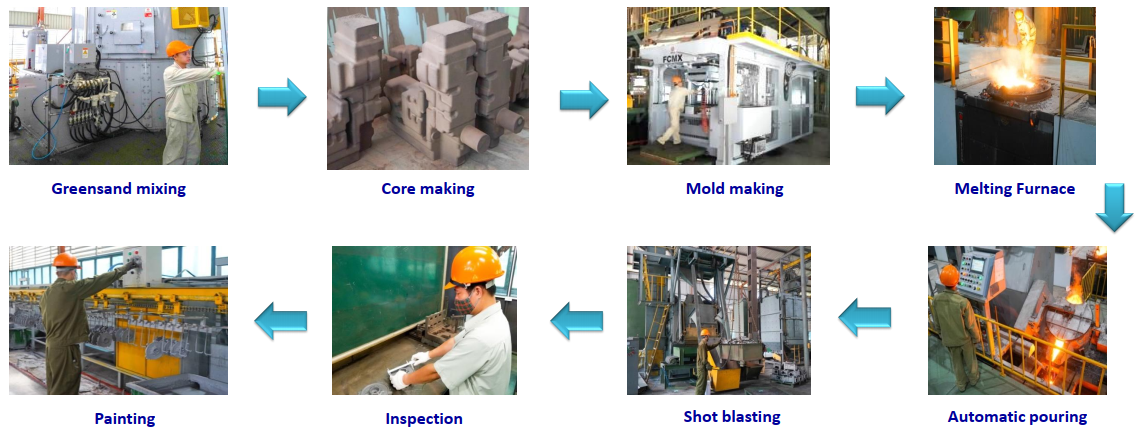
DISOCO employs an automatic sand casting system using SINTO (Japan) equipment, which helps stably control the mold-making process and enhance precision in mass production.Additionally, DISOCO utilizes casting simulation software to analyze metal flow, heat distribution, and shrinkage trends, thereby optimizing gating system design and reducing the risk of warping before actual production.Cooling and demolding processes are controlled according to standards to limit residual stress and maintain dimensional stability for castings.Furthermore, a quality control system with modern inspection equipment helps DISOCO early detect shape deviations and ensure precision for products requiring high tolerances.Thanks to the combination of Japanese technology, technical expertise, and strict process control, DISOCO helps customers:
- Reduce casting deformation
- Stabilize product dimensions
- Reduce post-casting correction costs
- Optimize mass production efficiency
Download DISOCO's Sand Casting Solutions Document
👉 Download the detailed document on DISOCO's sand casting solutions now to learn how to limit warping defects, control deformation, and enhance dimensional stability in mass production.
Company Information
Green sand casting components. / Burnt sample casting components. / Hot forging components
Our company specializes in casting, forging, stamping, heat treatment, mainly manufacturing engine parts. Currently, the company is conducting transactions with many Japanese enterprises, as well as p ...
PICKUP
Technology & Services
CONTACT
Contact