SERVICES
Technology & Services
Cast Iron Casting Process using Green Sand Molds: From Mold Creation to Final Machining at DISOCO

Technology & Services
Green Sand Casting – Foundational Manufacturing Technology for the Mechanical Engineering Industry
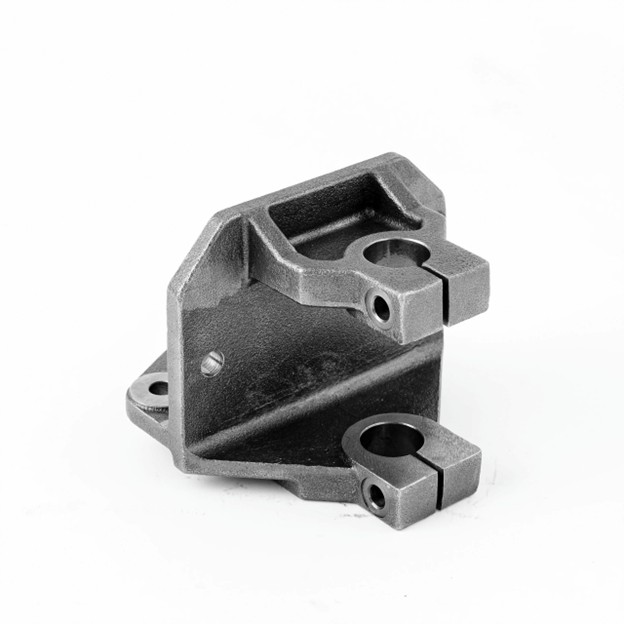
Green Sand Casting is one of the most widely used casting technologies in the mechanical manufacturing industry. Thanks to its flexibility in producing various types of parts with different shapes and sizes, this technology is widely applied in fields such as automotive, electric motors, industrial machinery, pumps, valves, and mechanical equipment. At Song Cong Diesel One Member Limited Liability Company (DISOCO), the green sand casting process is implemented on automatic and semi-automatic casting lines, combined with a quality control system and post-casting machining. Synchronized control of each stage helps the company produce gray cast iron (FC) and ductile cast iron (FCD) products that meet the quality, precision, and stability requirements of many domestic and international industries.
What is Green Sand Casting?
Green Sand Casting is a method of forming castings using molds made from a mixture of silica sand, bentonite, and water. After the molten iron is poured into the mold and solidifies, the sand mold is broken to retrieve the product. This technology is widely used due to its ability to produce a diverse range of products, from simple parts to complex structures. Additionally, the mold sand can be reused after processing, which helps optimize production costs and is suitable for both single-piece and mass production.
Key Components in the Casting Process
To create a complete cast iron product, the sand mold casting process uses three main components:
- Pattern: A replica of the product, used to form the mold cavity. After the mold is created, the pattern is removed and reused for subsequent production runs.
- Sand Mold: The mold that forms the external shape of the product. Molten iron is poured into the mold cavity and solidifies into this shape.
- Sand Core: Used when the product has internal holes or hollow cavities. The core is placed in the mold before pouring the iron and is broken out after the product solidifies to create the designed hollow structure.
Green Sand Casting Process at DISOCO

Step 1. Sand Mold Preparation and Treatment
The quality of the sand mold is a crucial factor determining the accuracy and surface quality of the casting. The mold sand mixture is blended from silica sand, bentonite, water, and additives in appropriate proportions to ensure strength, permeability, and stability during the casting process. At DISOCO, the sand treatment system operates synchronously to control sand quality before mold creation, contributing to the stability of each production batch.
Step 2. Core Making
For products with internal cavities, holes, or passages, sand cores are manufactured separately before being assembled into the mold. The sand core must ensure the correct design shape, sufficient strength during assembly and iron pouring, and be easily broken out after the product solidifies. To accommodate various product forms, DISOCO applies Shell Core and Phenix core-making technologies, enhancing the precision of complex structural parts.
Step 3. Mold Creation
Once the mold sand meets requirements, the pattern is placed in the flask, and the sand is compacted around it. When the pattern is removed, the remaining space forms the mold cavity, which has the shape of the desired casting. At DISOCO, this stage is performed on an automatic sand molding line from SINTO (Japan), which increases productivity, uniformity, and stability of each mold.
Step 4. Core Setting and Mold Assembly
After mold creation, the sand cores are placed in the correct positions according to technical drawings to create internal cavities or passages in the product. The two mold halves are then tightly assembled, secured, and inspected before moving to the metal pouring stage.
Step 5. Iron Melting and Alloying
Raw iron is melted in an induction furnace to the appropriate temperature before being poured into the mold. Throughout this process, the chemical composition and metal temperature are controlled to ensure the correct material grade as required. DISOCO currently produces gray cast iron (FC) and ductile cast iron (FCD) products, and performs chemical composition analysis using a specialized system before pouring.
Step 6. Iron Pouring into the Mold
Molten iron is introduced into the mold cavity through the gating system. The metal fills the entire mold cavity and surrounds the sand core to form the complete shape of the product. DISOCO uses an automatic pouring system, which helps to stably control the amount of metal, temperature, and pouring speed, reducing defects such as misruns, gas entrapment, or slag inclusions.
Step 7. Cooling and Solidification
After pouring, the molten iron begins to solidify in the mold. The cooling time is calculated to suit the size, thickness, and structure of each product to ensure mechanical properties and minimize deformation.
Step 8. Mold Breakout and Casting Retrieval
Once the product has completely solidified, the sand mold is broken to retrieve the casting. For products using sand cores, the internal core is also broken out to create the designed hollow cavities or passages.
Step 9. Cleaning and Shot Blasting
After mold breakout, the product is further:
- Cut off from the gating system and risers.
- Deburred.
- Shot blasted to remove sand and oxide layers from the surface.
This stage helps improve surface quality before moving on to inspection or machining.
Step 10. Quality Inspection
Before shipment, products are inspected according to technical criteria such as:
- Chemical composition.
- Mechanical properties.
- Dimensions.
- Appearance.
- Surface and internal defects (when required).
Throughout the process, quality control ensures that products meet customer requirements across various industrial sectors.
Step 11. Machining and Product Finishing
In addition to supplying cast iron blanks, DISOCO also performs post-casting machining stages such as:
- CNC turning.
- CNC milling.
- Drilling, reaming.
- Grinding.
- Surface treatment.
- Finish painting.
This allows customers to choose from cast blanks to fully machined parts, helping to shorten production time and optimize the supply chain.
DISOCO's Green Sand Casting Capabilities
With many years of development in the cast iron industry, DISOCO has invested comprehensively in its green sand casting lines, melting systems, quality control, and post-casting machining, meeting the production needs from cast blanks to finished parts for various industries. Some of DISOCO's outstanding capabilities include:
1. Automatic Green Sand Casting System
✔ SINTO Line (Japan) ✔ Capacity: 10,000 tons/year ✔ Molding Speed: 30 seconds/mold ✔ Flask Size: 700 × 600 × 500 mm ✔ Melting Furnace System:
- 01 pair of 1 ton/batch furnaces
- 01 pair of 1.5 ton/batch furnaces
✔ Product Weight: 1 – 70 kg
2. Semi-Automatic Green Sand Casting System
✔ Capacity: 5,000 tons/year✔ Molding Technology: Green Sand (Sand + Bentonite)✔ Core Making Technology:
- Shell Core
- Phenix
✔ Product Weight: 1 – 100 kg
3. Comprehensive quality control system, from mold sand control, chemical composition analysis, mechanical property testing, metallographic examination to dimensional inspection and non-destructive testing (NDT), ensuring stable quality for each product.
4. Post-Casting Finishing: Providing everything from cast iron blanks to fully machined parts according to customer requirements
If your business is looking for a partner to produce cast iron products using green sand casting technology, DISOCO is ready to accompany you from technical consultation and material selection to production and complete finishing as required.
Company Information
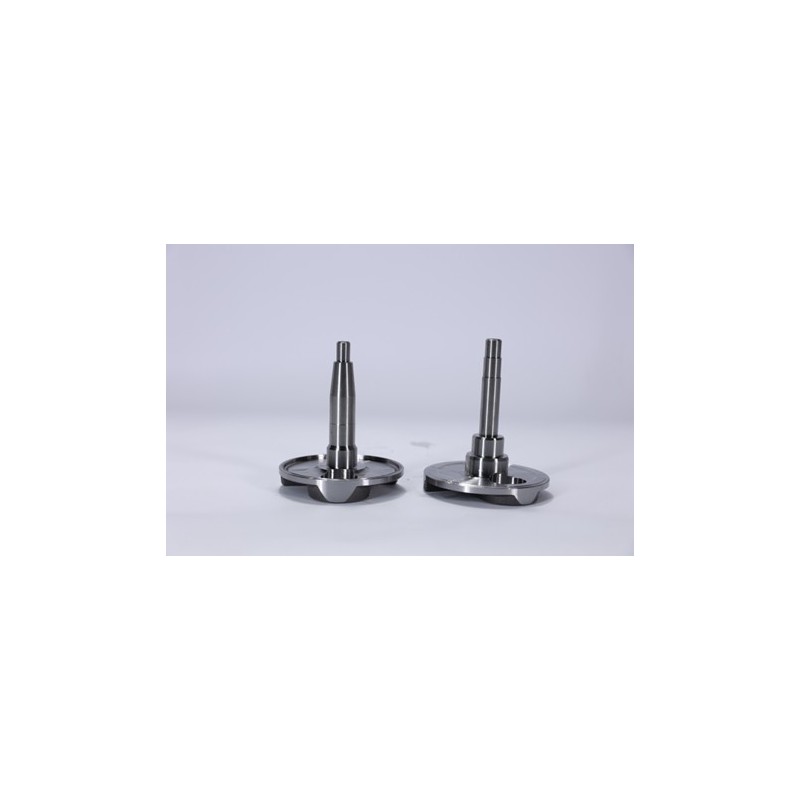
Green sand casting components. / Burnt sample casting components. / Hot forging components
Our company specializes in casting, forging, stamping, heat treatment, mainly manufacturing engine parts. Currently, the company is conducting transactions with many Japanese enterprises, as well as p ...
PICKUP
Technology & Services
CONTACT
Contact